
Bajaj Masterbatch · PP fibrillated yarn
Engineered to split.
Designed to perform.
PP-based masterbatch solutions for consistent colour, controlled fibrillation and application-specific protection in polypropylene split-film yarn.
The material
One oriented tape.
A network of possibilities.
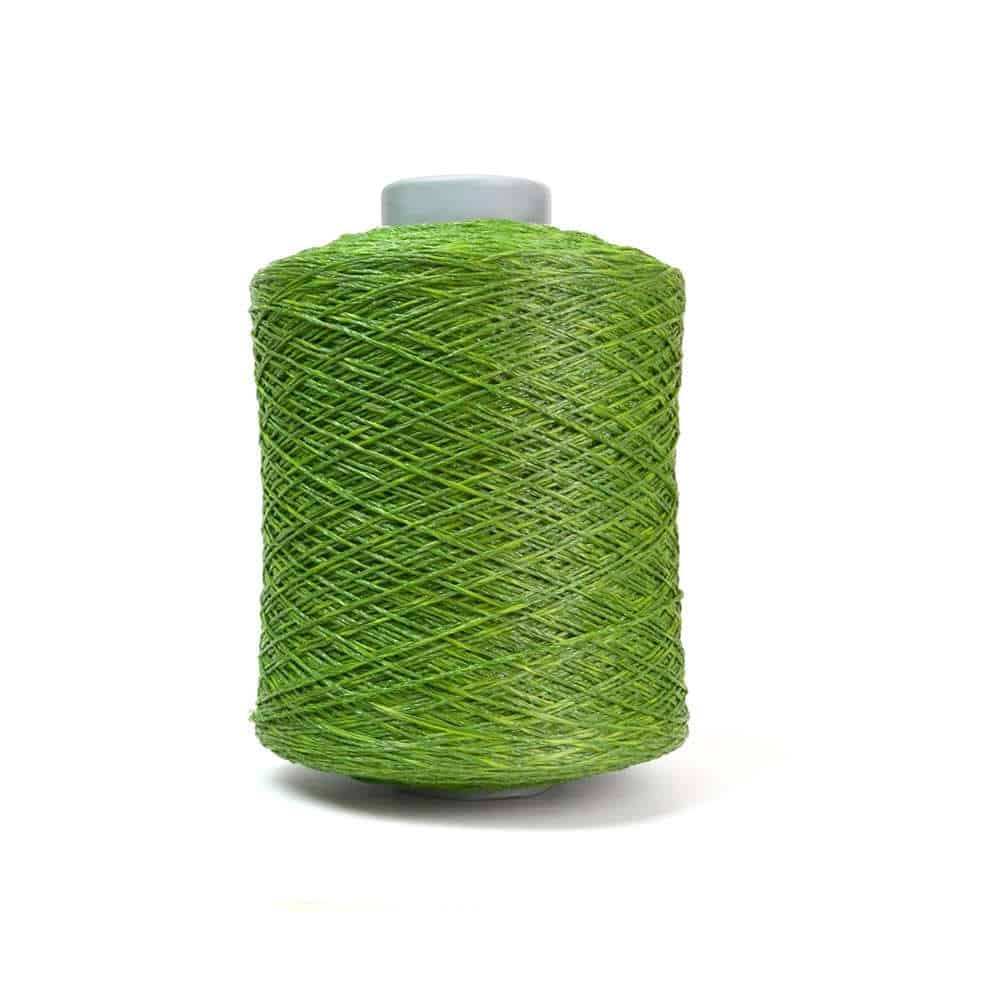
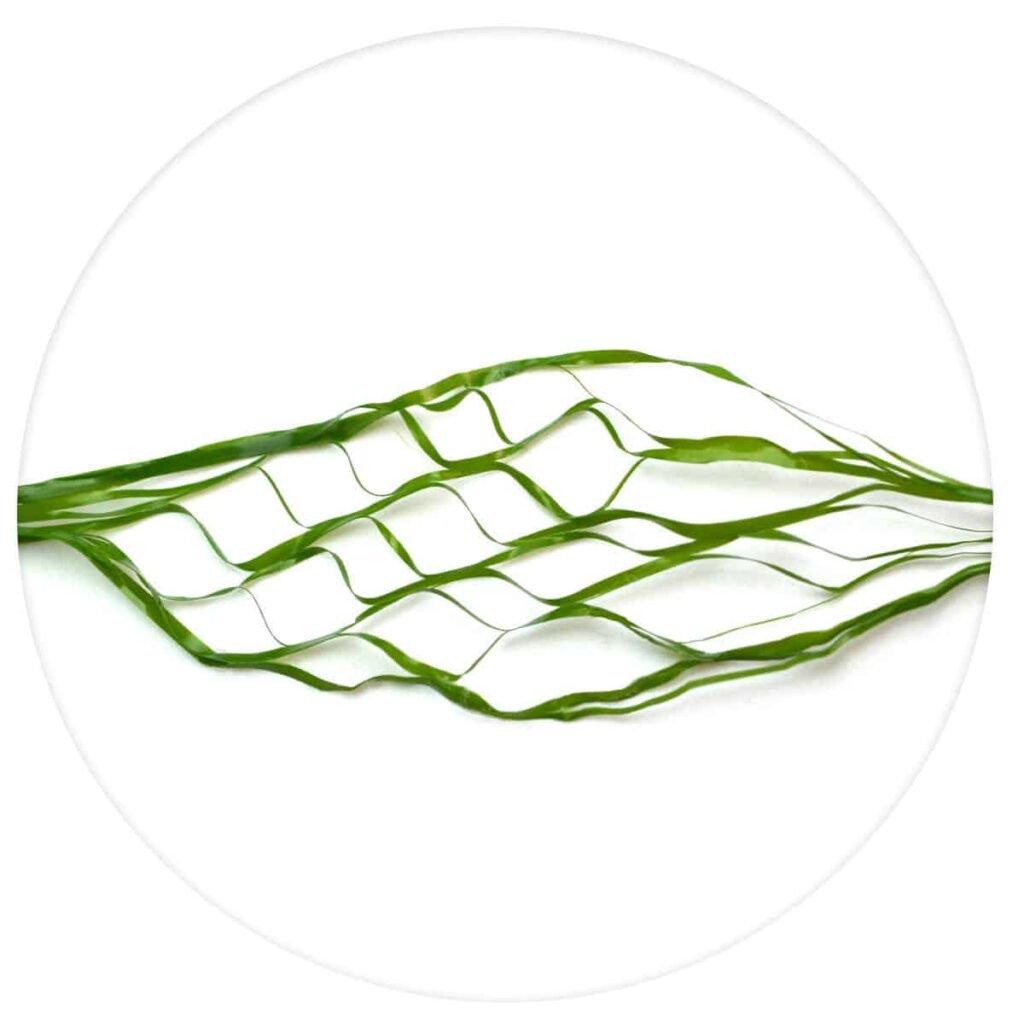
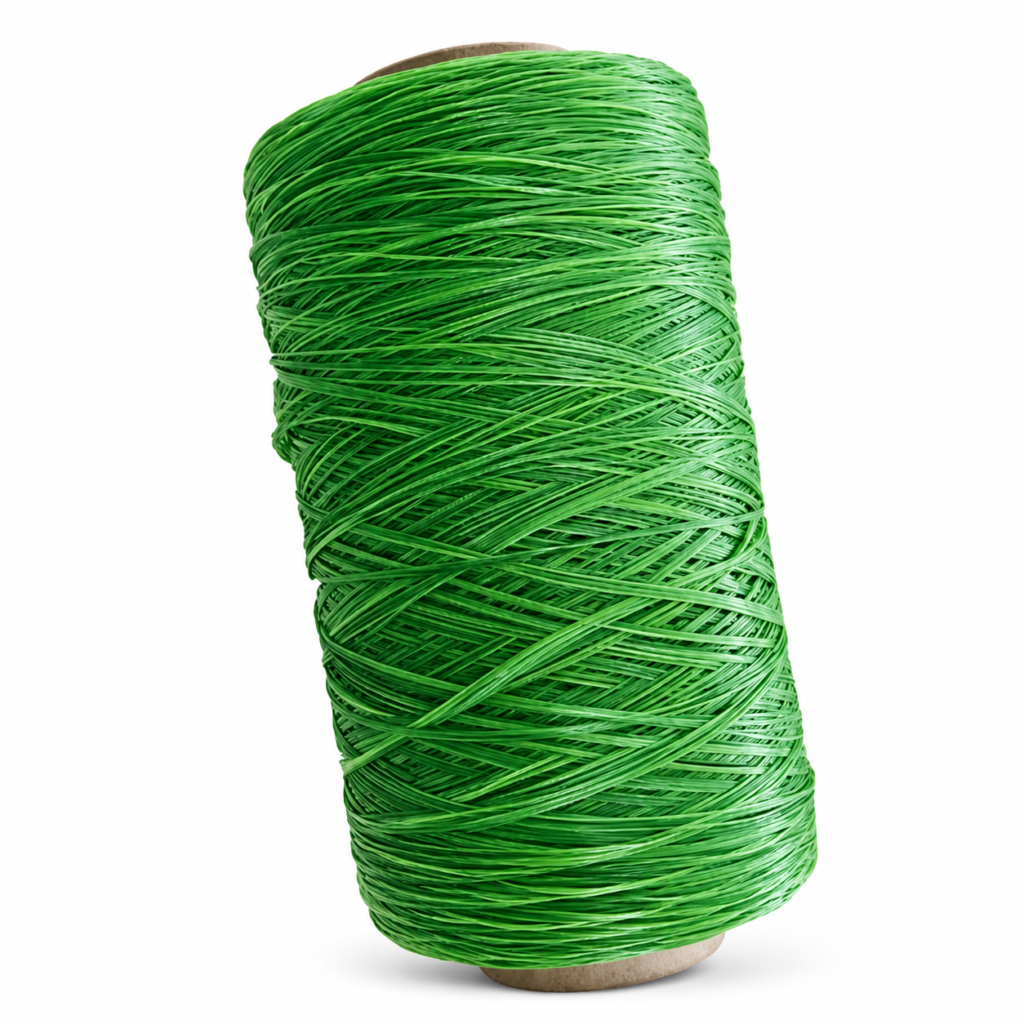
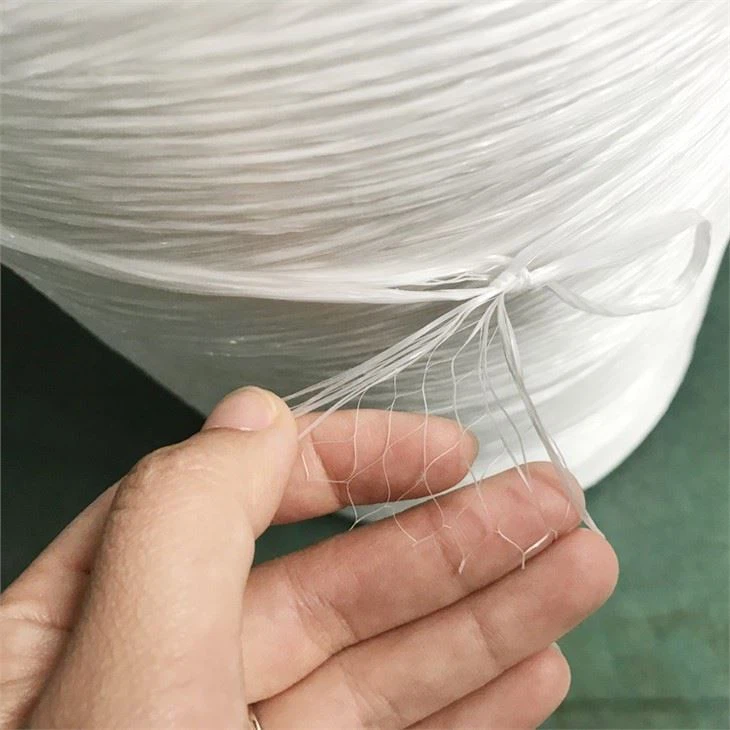
PP fibrillated yarn is produced by mechanically splitting an oriented polypropylene film tape into an interconnected network of fine strands.
Strength begins before splitting.
Extrusion forms the film. Slitting defines tape width. Hot drawing aligns the polymer chains in the machine direction. A fibrillating unit then creates controlled longitudinal splits while retaining interconnected bridges.
The final balance of linear density, tenacity, elongation, shrinkage and mesh opening depends on resin selection, additive dispersion and line settings—not the masterbatch alone.
Features & benefits
Small additions.
Meaningful material control.
Uniform colour
Well-dispersed PP colour concentrates help limit pigment streaks and visible shade variation across tapes and wound packages.
Drawability matters
Fine dispersion reduces agglomerate-related stress concentration during orientation, supporting a stable drawing and fibrillation window.
Outdoor resilience
An application-matched PP UV package helps slow photo-oxidative chain scission, embrittlement and loss of mechanical properties.
Cleaner visual finish
White and optical brightener options adjust opacity and perceived whiteness for yarns where appearance is a purchase criterion.
Controlled economics
A qualified PP filler formulation can adjust stiffness, opacity and compound cost. Loading must preserve the required split pattern and strength.
Repeatable conversion
Consistent concentrate feeding and carrier compatibility support reproducible processing, winding and downstream conversion.
Purposeful fibrillation
A controlled network.
Not random damage.
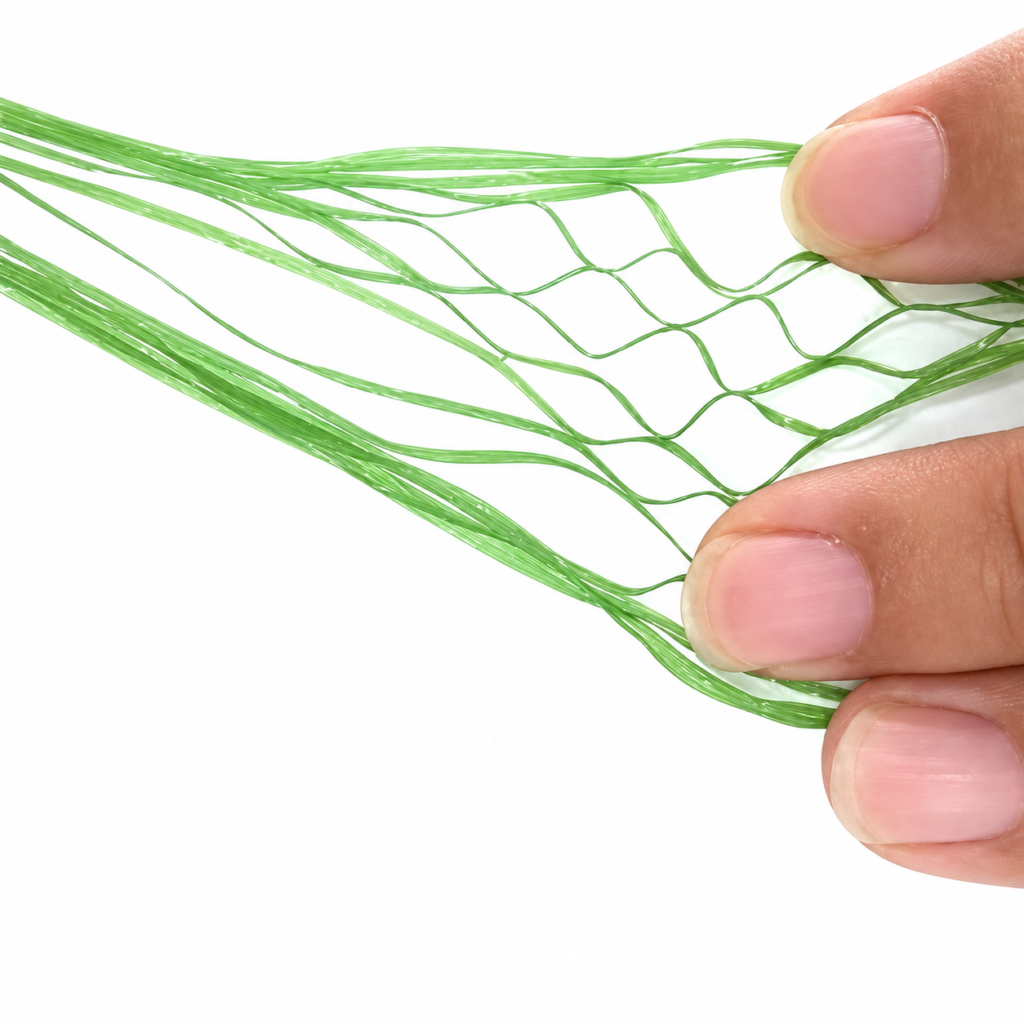
The split pattern is a specification.
Fibrillator pin geometry, penetration, contact angle, relative roller speed and tape tension influence the number and extent of splits. Drawing history and tape thickness determine how that network develops.
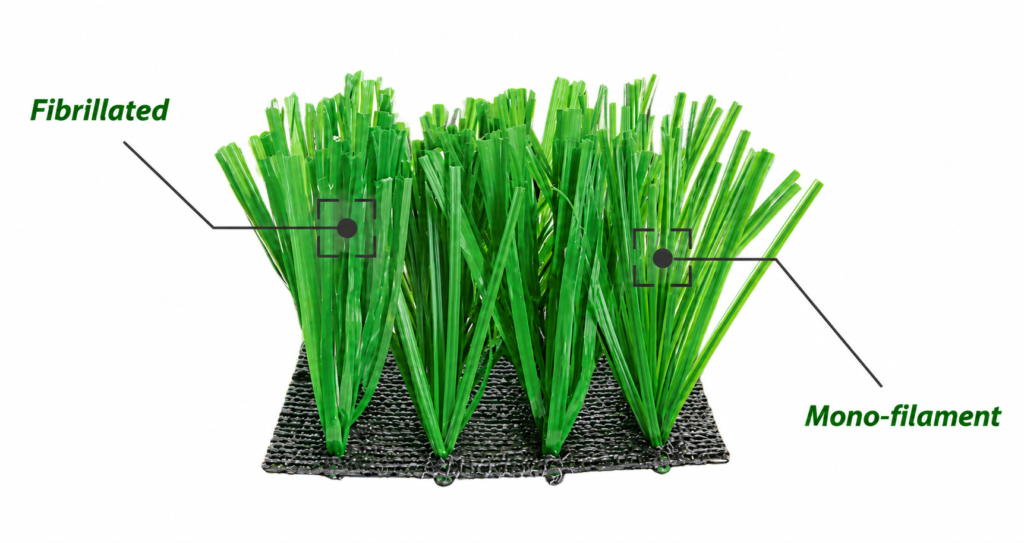
Random edge cracking, broken bridges, powder and excessive strand separation indicate an unstable material or process balance. A masterbatch promoted for anti-fibrillation in woven tapes must not automatically be selected for yarn intended to fibrillate.
Manufacturing process
From PP granules.
To engineered yarn.
A typical split-film route uses flat-die film extrusion, tape orientation and mechanical fibrillation. Equipment configuration can change the sequence of heat setting and splitting.

Meter & blend
Meter PP resin and PP-carrier concentrates gravimetrically where possible. Keep the blend clean and control recycled content, contaminants and pellet segregation.
Extrude & filter
Melt and homogenise the formulation, filter contaminants and extrude a uniform film through a flat die. Monitor melt temperature, pressure and screen-pressure rise.
Quench & slit
Cool the film consistently and slit it into tapes. Film gauge and slit width set the starting mass per length; damaged blades can create edge defects.
Heat & draw
Stretch tapes between controlled-speed rollers through a heated zone. Draw ratio and temperature establish orientation, tenacity and elongation.
Fibrillate & stabilise
Pass oriented tape through a pin or needle fibrillator to form connected strands. Optimise heat setting or relaxation to control residual shrinkage.
Wind & convert
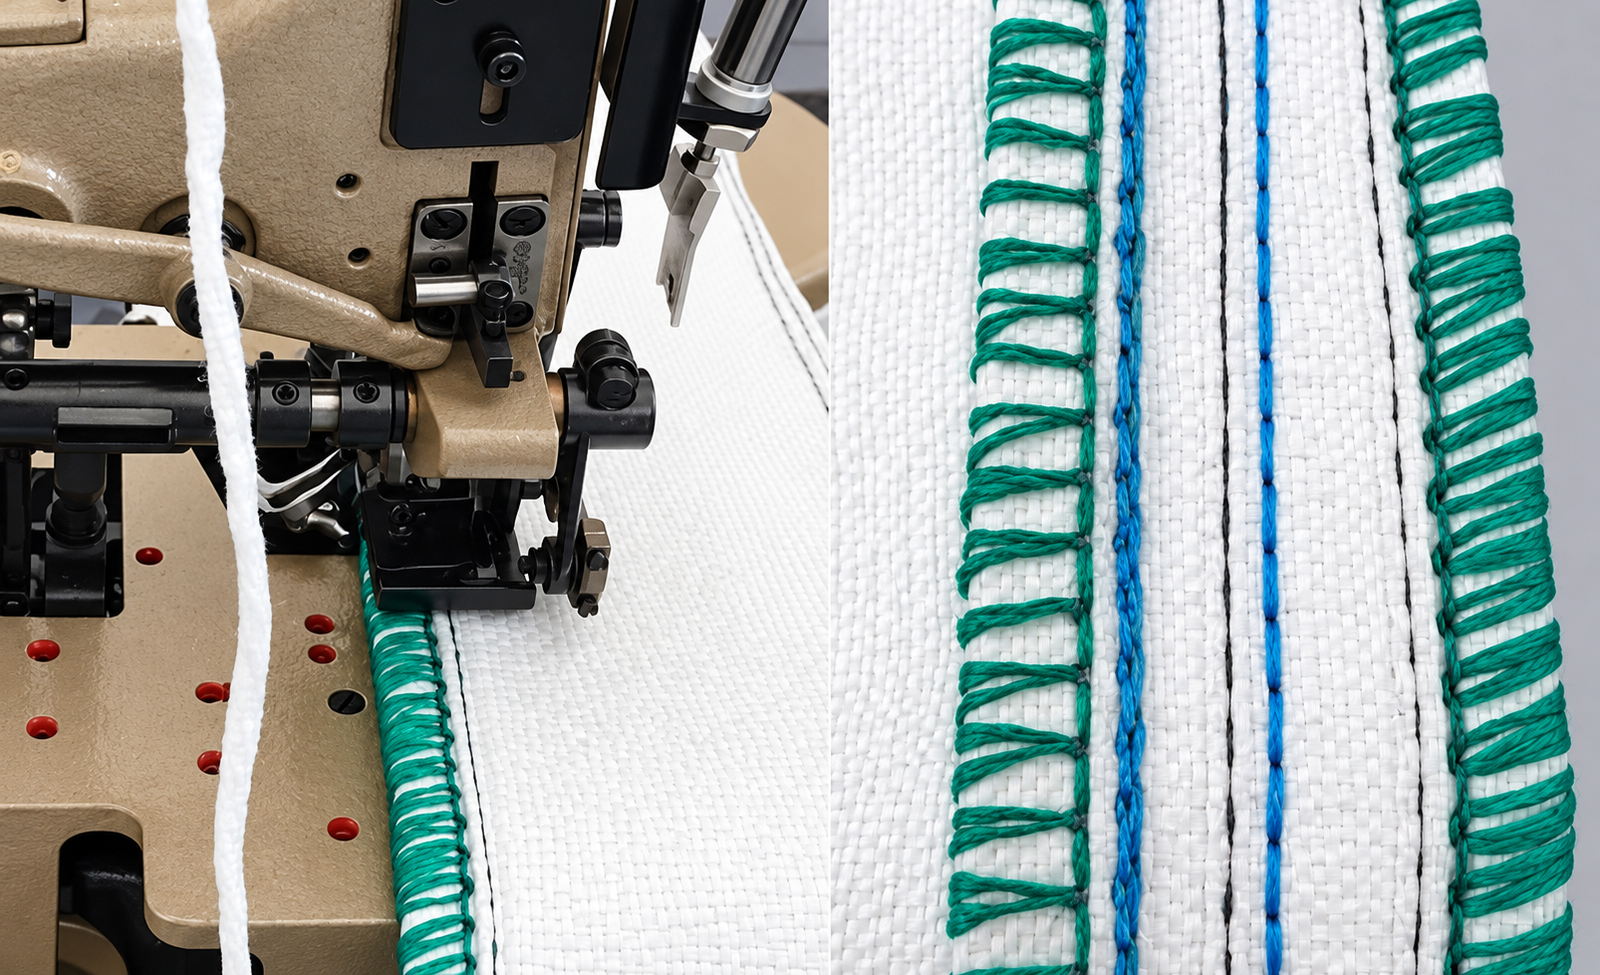
Wind under controlled tension; twist or assemble when required. Check package build, yarn handling and performance in tufting, rope making or other conversion.
Set temperatures, draw ratios and speeds from the PP resin supplier’s guidance and actual line trials. A universal processing recipe is not appropriate across yarn sizes, formulations and machines.
On the production floor
Consistency at every stage.
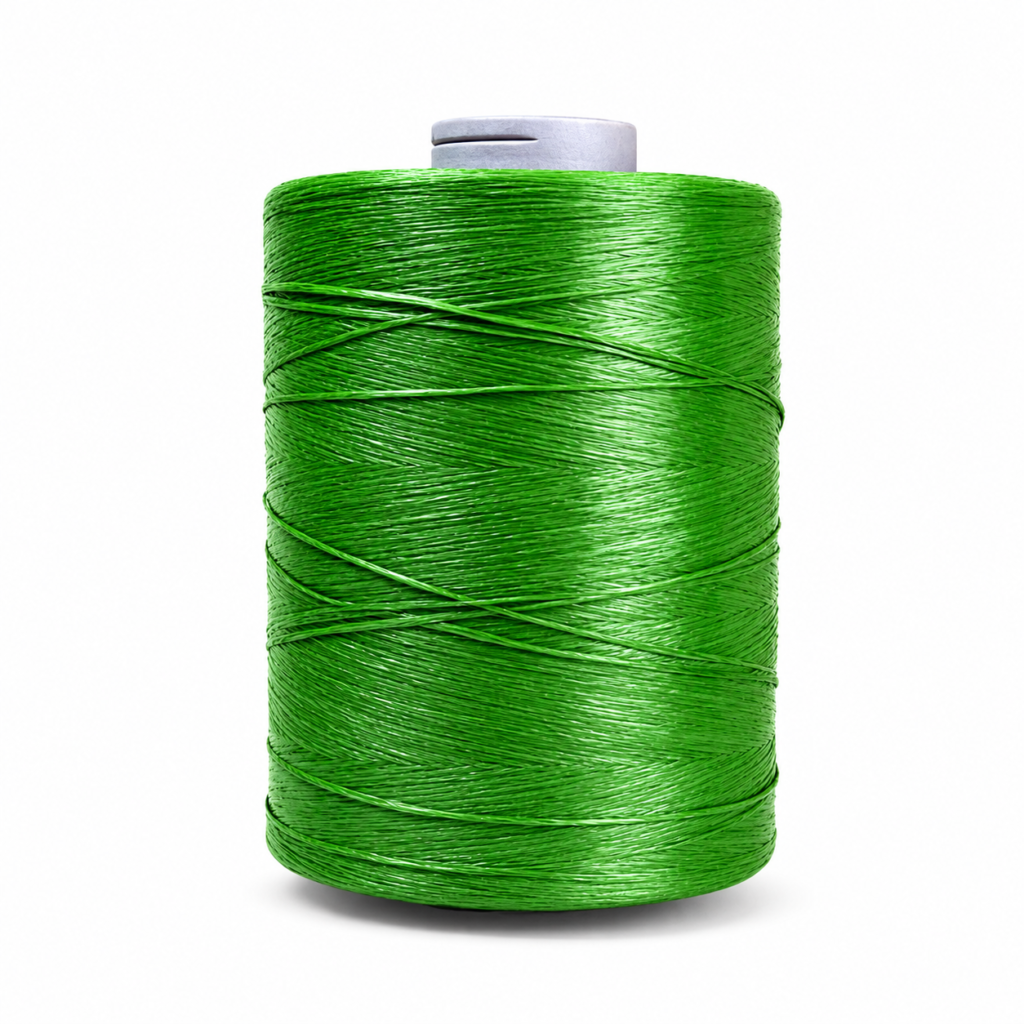
Dispersion is a process parameter.
Inadequately dispersed pigment or mineral particles may initiate local failure during drawing. Evaluate masterbatch filtration behaviour and dispersion at the actual melt temperature, screen arrangement and draw ratio.
Match carrier melt behaviour to the PP system. Record dosing accuracy, torque, melt pressure, film gauge, tape breaks and fibrillator settings to separate formulation effects from mechanical causes.
Bajaj PP masterbatch range
The right concentrate.
For the right yarn.
Build the formulation around the required function. Specify PP carrier resin explicitly when requesting a grade.
 Outdoor applications
UV stabilizer masterbatch
Specify a PP-carrier PLAST UV grade. HALS-based stabilisation helps interrupt photo-oxidation and supports property retention in exposed turf, ropes and technical yarns. Select the package for pigment chemistry and service environment.
Explore product family ↗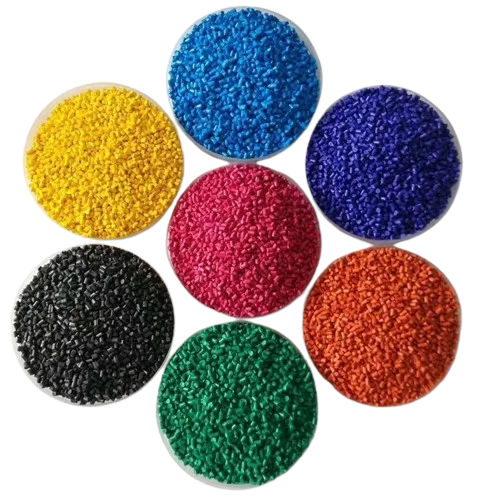 Shade & appearance
Colour masterbatch
PP-carrier PLAST COLOUR concentrates provide shade control. Specify pigment heat stability, dispersion, light fastness and migration performance for the actual end use; qualify changes in colour against drawing behaviour.
Explore product family ↗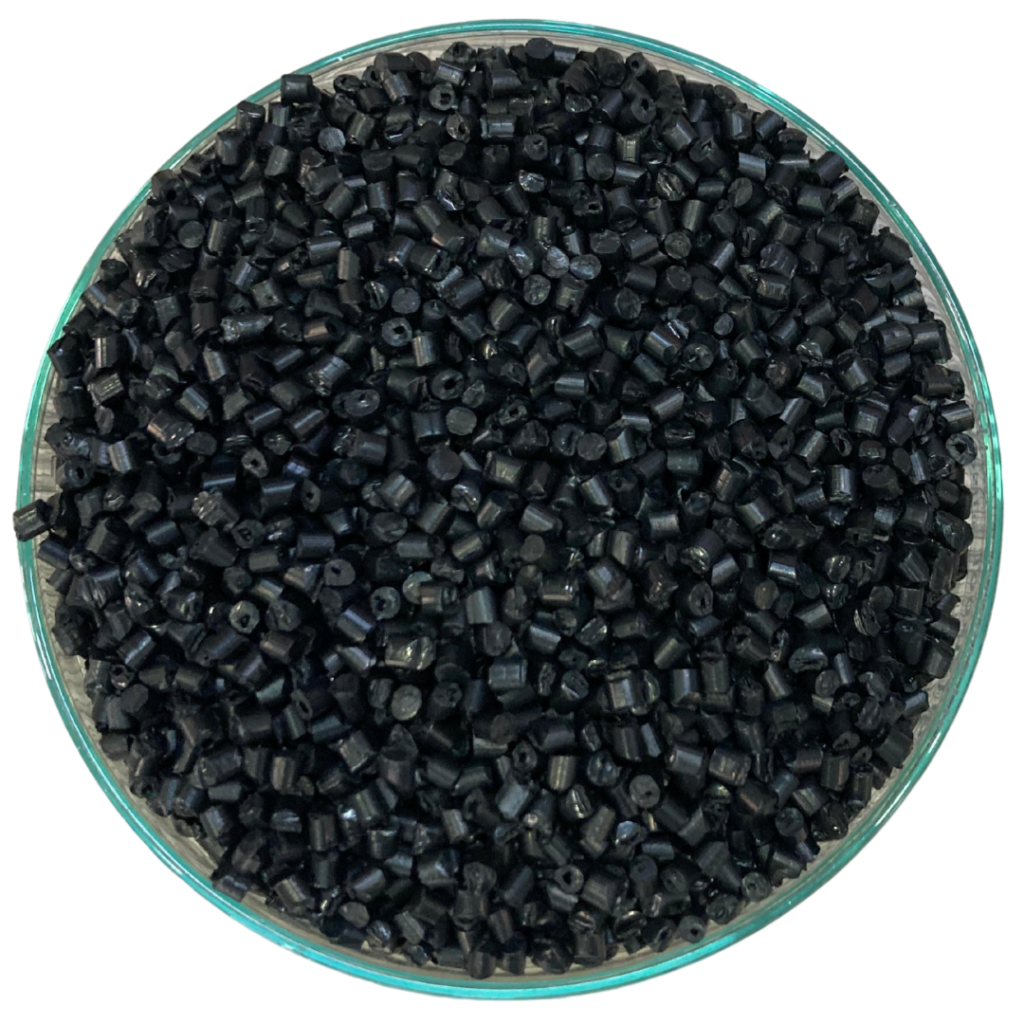 Black yarn formulations
Black masterbatch
Select a PP-carrier black grade with dispersion suited to drawn tapes. Carbon black provides colour and can contribute UV screening; outdoor durability still requires validation of loading, dispersion and the complete stabiliser system.
Explore product family ↗ Conditional cost optimisation
PP filler masterbatch
Evaluate a PP-base mineral concentrate only where the yarn specification permits it. Particle size, top-cut, treatment and loading influence drawability, abrasion, dust, density and fibrillation. PLAST FAB or PLAST STIFF selection requires a yarn-specific trial.
Explore product family ↗ White & natural yarn
Optical brightener masterbatch
Specify a PP-carrier optical brightener such as a qualified PLAST BRIGHT grade to adjust perceived brightness. It complements white pigment when required; it does not replace TiO₂ opacity or UV stabilisation.
Explore product family ↗White yarn? Add the right white.
For opaque white yarn, request a PP-carrier TiO₂ white masterbatch. Evaluate whiteness, undertone, dispersion and the interaction with the UV package. TiO₂ loading and pigment treatment must be selected for the required appearance and drawing performance.
For demanding heat histories, discuss an antioxidant concentrate to support processing stability. Antistatic, slip, antimicrobial or flame-retardant additives are specialised options only when the end-use specification calls for them; each needs separate qualification.
Explore white masterbatches ↗
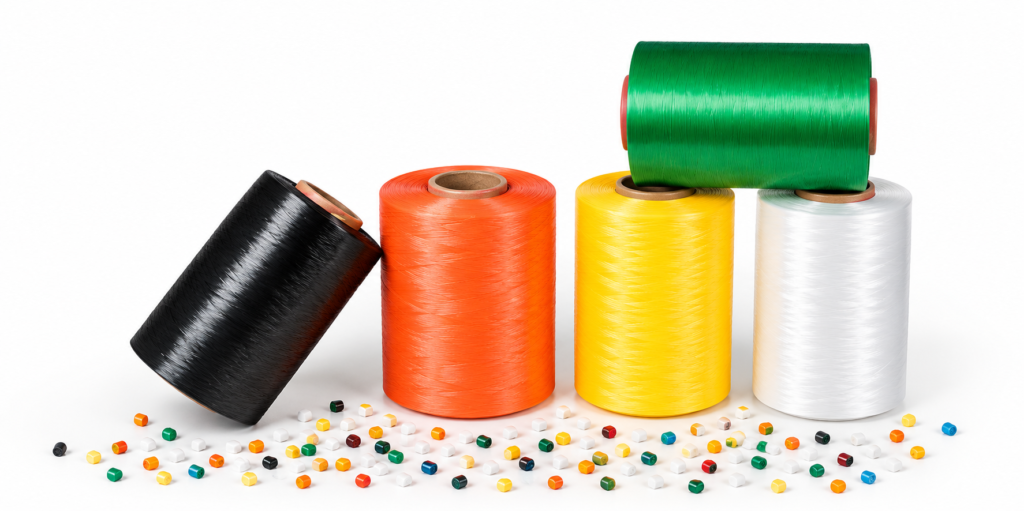
The five masterbatch photographs above are from Bajaj’s PP monofilament yarn page and illustrate product families. They do not independently confirm carrier resin or suitability of every grade. Confirm current TDS, PP carrier, recommended dosage and yarn trial results with Bajaj before production.
Application-led selection
Start with the end use.
| End use | Masterbatch priorities | Validate on finished yarn |
|---|---|---|
| Artificial turf & landscaping | PP colour + PP UV; PP black where required | Colour retention, tensile retention after weathering, split pattern and tufting behaviour |
| Rope, twine & cordage | PP colour or black; PP UV for outdoor use | Tenacity, elongation, twist response, knot behaviour and abrasion |
| Cable filler yarn | PP colour or white when specified; other additives only to cable requirements | Linear density, bulk, shrinkage and compatibility with the cable construction |
| Industrial & technical yarn | PP colour, white or black; UV and antioxidant as required | Package consistency, thermal shrinkage and downstream conversion |
| Concrete reinforcement fibres | Project-specific colour and stabilisation; qualified formulation | Cut length, dispersion in the mix and performance against the applicable fibre specification |
Qualification & quality
Measure performance.
Then scale with confidence.
Yarn mechanics
Measure linear density, breaking force, tenacity and elongation using an appropriate yarn tensile method such as ISO 2062 or ASTM D2256, where applicable.
Network geometry
Compare mesh opening, split distribution, bridge integrity and loose strands at controlled draw and fibrillator settings.
Thermal stability
Measure shrinkage under the intended time and temperature conditions. Inspect for yellowing, gels and changes in drawing response.
Colour consistency
Agree shade tolerances and a measurement method on representative yarn or standardised plaques. Assess pigment heat and light stability.
Outdoor testing
Choose accelerated weathering appropriate to the service environment, then assess retained strength and colour. Test hours do not directly equal years outdoors.
Line economics
Track break frequency, filter-pressure rise, output, waste and conversion yield. Compare cost per acceptable finished product rather than concentrate price alone.
Troubleshooting
A better yarn starts
with a better diagnosis.
| Observation | Check first | Formulation response |
|---|---|---|
| Breaks during drawing | Gauge variation, draw temperature, resin degradation, slit edges | Check pigment/mineral dispersion; review filler loading and carrier suitability |
| Irregular splitting | Fibrillator wear, pin penetration, relative speed and tension | Review tape orientation and additive effects on splitting; trial one change at a time |
| Powder or loose fibrils | Over-fibrillation, abrasion and mineral particle characteristics | Reduce unsuitable filler loading; review mineral grade and dispersion |
| Shade streaks | Dosing variation, pellet segregation and mixing | Review pigment strength, carrier rheology and concentrate dispersion |
| Outdoor embrittlement | Exposure, formulation, pigment interactions and stabiliser consumption | Requalify PP UV package and loading with weathering plus tensile testing |
Why choose Bajaj Masterbatch
Material knowledge.
Application focus.
A coordinated approach to colour, additives and processing—built around the performance your yarn must deliver.
A broad product basket
Access Bajaj colour, white, black, UV, optical brightener and PP filler families to address different formulation needs.
PP-focused selection
Ask for carrier confirmation and a concentrate suited to tape extrusion, hot drawing and controlled fibrillation.
Technical collaboration
Share your resin, line configuration, yarn size and end-use targets so the recommended formulation can be assessed under relevant conditions.
Yarn possibilities
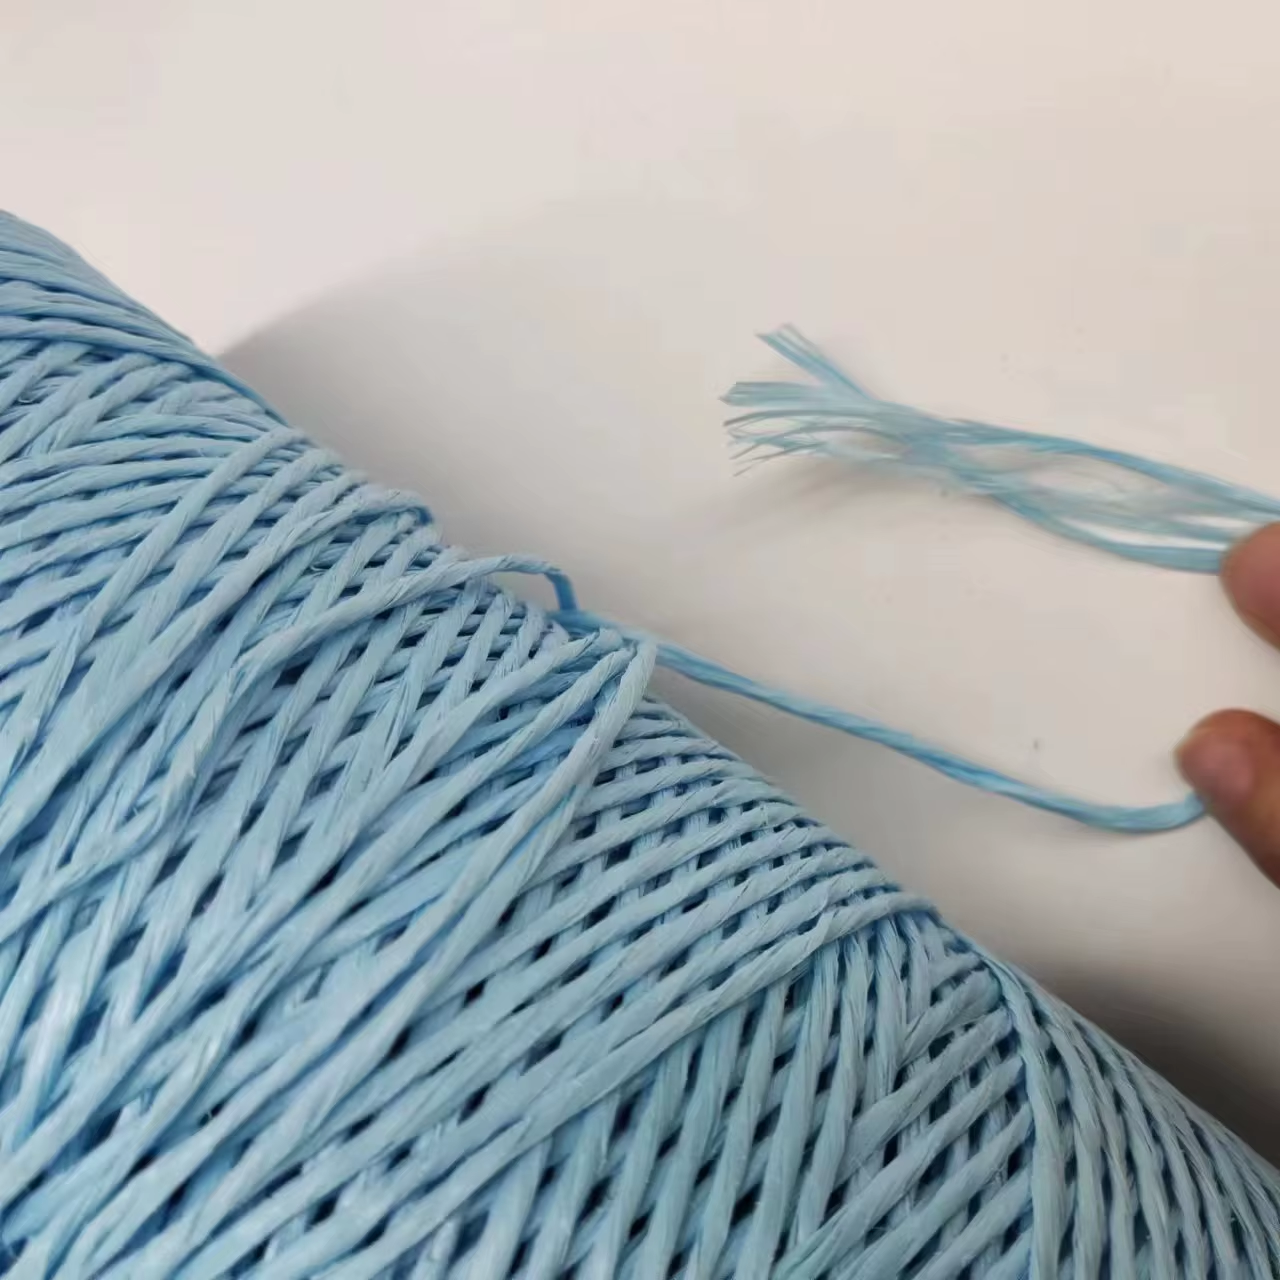
Colour. Texture.
Technical purpose.
Frequently asked questions
The details that matter.
Which masterbatches are essential?
There is no universal package. Colour, white or black is selected for appearance; PP UV is important for exposed applications. Filler, optical brightener, antioxidant and other additives depend on the yarn specification.
Why specify a PP carrier?
A PP carrier aligns the concentrate with the base polymer system. Carrier rheology and dispersion still need checking because carrier identity alone does not establish suitability for high-draw tape processing.
Can filler be used in fibrillated yarn?
Sometimes, after qualification. Mineral addition changes density, drawing and splitting behaviour. Optimise loading against tenacity, elongation, dust, mesh quality and conversion performance; avoid assuming a woven-sack formulation will transfer unchanged.
What dosage should be used?
Use the current grade TDS and a controlled line trial. Active concentration, pigment strength, yarn size, resin, exposure and the rest of the additive package determine the required loading.
Is fibrillated yarn made through a spinneret?
The conventional split-film route starts with extruded film that is slit, drawn and mechanically fibrillated. Monofilament and multifilament yarns use different extrusion geometries and should not be treated as identical processes.
Let’s develop your formulation
Tell us your yarn.
We’ll help select the package.
Share the PP grade, yarn dtex or denier, shade, draw ratio, end use, outdoor exposure and performance targets. Request a PP-carrier recommendation, current TDS and a trial plan.